
6 Best Coolants For Drilling Stainless Steel For Workshops
Struggling to drill stainless steel? Discover the 6 best coolants to extend tool life and improve finish in your workshop. Click here to optimize your process.
Drilling into stainless steel is the quickest way to ruin a perfectly good drill bit if the right preparation is ignored. It is a stubborn, work-hardening material that laughs at the high-speed steel bits commonly found in most hobby farm workshops. Choosing the right coolant changes the job from a frustrating battle of burned edges into a smooth, precise operation.
Disclosure: As an Amazon Associate, this site earns from qualifying purchases. Thank you!
CRC TrueTap: Best Overall for Tough Metals

When a project demands drilling through thick stainless steel plate for a tractor implement repair, CRC TrueTap is the gold standard. This formula is specifically engineered to cling to vertical surfaces, preventing the fluid from running off before it can actually reach the cutting edge. It excels at reducing friction, which is the primary enemy when working with stainless steel.
The heavy-duty nature of this fluid makes it ideal for the occasional but high-stakes shop task. Because it minimizes heat buildup, the drill bit stays sharp significantly longer, preventing the work-hardening effect where the steel becomes harder as the bit rubs against it.
If the workshop stock consists of a variety of stainless alloys and thicknesses, reach for this bottle. It provides the consistency needed to drill clean holes without the constant need to stop, cool, and regrind bits.
Tap Magic EP-Xtra: Pro-Grade Performance

Tap Magic EP-Xtra is a thin, high-performance fluid that penetrates deeply into the microscopic space between the drill bit and the stainless steel. Its standout feature is its ability to dissipate heat rapidly, which is essential when drilling deep holes or using larger diameter bits.
Unlike thicker oils that might sit on the surface, this fluid flows directly into the flutes of the drill bit. This ensures the cutting edges stay lubricated throughout the entire duration of the hole creation.
This product is highly recommended for users who prioritize speed and efficiency in their workflow. It is the go-to choice for those who want professional-grade results on stainless steel without needing specialized machinery.
Boelube Paste: The No-Drip, No-Mess Option

For tasks involving overhead drilling or working on sensitive equipment where dripping oil is a major concern, Boelube Paste offers a unique solution. It stays exactly where it is applied, creating a consistent film that does not splatter or run.
The paste excels in precision work where drill bits are small and delicate. Because it is a non-toxic, synthetic lubricant, it provides exceptional lubricity without the heavy odor often associated with sulfurized cutting oils.
Opt for this if the shop environment needs to remain clean or if the drill press is positioned over other equipment that shouldn’t be covered in oil. It is a reliable, mess-free alternative that performs exceptionally well on stainless alloys.
Relton A-9: Surprisingly Great on Stainless

While many know Relton A-9 for its performance on aluminum, its performance on stainless steel is an underrated asset. It is a highly effective cutting fluid that prevents the sticky, gummy chips that usually cause drill bits to grab and snap.
The formulation allows for a cleaner cut, leaving the hole edges smooth rather than ragged. It works by reducing the torque required to force the bit through the material, which helps in preventing bits from binding.
This is a fantastic “all-purpose” choice for the hobby farm workshop. Keep a bottle on the shelf to cover stainless steel tasks while knowing it remains just as effective for other metals encountered during daily repairs.
Oatey Dark Cutting Oil: A Versatile Choice
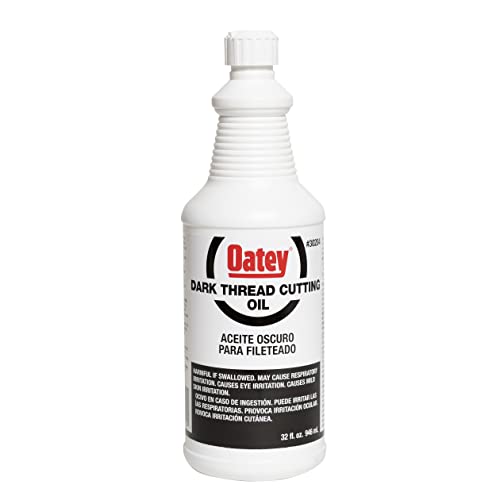
Oatey Dark Cutting Oil is a classic staple that has found its way into countless workshops due to its sheer reliability and accessibility. It is a thicker, sulfurized oil designed specifically to handle high-pressure contact between metal surfaces.
It is particularly useful for slower-speed drilling operations, such as when using a hand drill or a slow-geared bench drill press. The dark, heavy oil creates a visible barrier that makes it easy to see where the lubricant has been applied.
If the workshop budget is tight and the need for a versatile lubricant that can handle pipe threading as well as stainless steel drilling is a priority, this is the smart choice. It is a workhorse fluid that rarely fails to perform when used correctly.
Anchorlube G-771: Eco-Friendly Water-Based

Anchorlube G-771 represents the shift toward safer, water-based lubricants that don’t sacrifice cutting performance. It is essentially an emulsion that combines the cooling properties of water with the lubricating power of specialized additives.
This fluid is highly effective for stainless steel because it keeps the material cool enough to prevent the transformation that leads to work-hardening. Since it is water-soluble, cleanup is as simple as wiping the surface with a damp cloth.
Choose this product if the workshop is also used for food preparation areas or if there is a desire to minimize harsh chemicals in the shop environment. It offers a balanced, environmentally conscious approach to drilling tough, resistant alloys.
Why Stainless Steel Demands a Good Coolant
Stainless steel is deceptive; it is tough, but its biggest flaw is its tendency to harden when heated. When a drill bit rubs against the metal without cutting, the steel surface immediately increases in hardness, essentially creating a shield that the bit cannot penetrate.
This is why “cool” is just as important as “lubricate.” A good coolant conducts heat away from the drill bit while simultaneously reducing the friction that generates that heat in the first place. Without coolant, even a high-quality cobalt bit will dull in seconds.
Fluid, Paste, or Spray: Which Type is Best?
- Fluids: Best for heavy-duty drilling, deep holes, and situations where the bit can be constantly flooded.
- Pastes: Ideal for overhead work, small precision holes, or when mess prevention is a priority.
- Sprays: Convenient for quick, occasional tasks, though they often lack the heat-wicking capacity of thicker fluids.
The choice should depend on the setup and the orientation of the workpiece. If the drill press allows for it, a thick fluid or oil is almost always superior for long-term bit health.
Proper Coolant Application for a Clean Hole
Simply splashing coolant on the surface of the stainless steel is rarely enough. The goal is to get the lubricant into the flutes of the bit so it can be carried down to the cutting tip.
Apply the coolant before starting the drill and periodically clear the chips out of the hole to reapply. If the drill begins to screech or smoke, stop immediately, clear the metal shavings, and apply more fluid before continuing.
Safety Tips for Handling Cutting Fluids
Even the most “eco-friendly” cutting fluids are not intended for human consumption or prolonged skin contact. Always wear nitrile gloves to prevent the fluid from being absorbed into the skin.
Ensure the workspace is well-ventilated, especially if the friction of the drill causes the oil to smoke. Finally, store all rags soaked in cutting oil in a sealed metal container, as some sulfurized oils can pose a spontaneous combustion risk when bunched together.
Effective drilling on the hobby farm is less about raw power and more about managing the physical properties of the materials. By selecting a high-quality coolant, maintaining a steady pressure, and keeping the drill bit sharp, the most stubborn stainless steel projects become routine maintenance. Stick to the right lubricant for the job, and the shop equipment will remain productive for years to come.
Frequently Asked Questions (FAQs)
What does coolant do when drilling stainless steel in a workshop?
Coolant for drilling stainless steel reduces thermal buildup at the cutting edge and lubricates chips to prevent work hardening. Stainless alloys like 304 and 316 conduct heat poorly, sending up to 80 percent of cutting friction directly into drill bits. Applying coolant flushes metal chips out of the flutes, protecting high-speed steel and cobalt drills from rapid thermal dulling. Without coolant, the material hardens instantly, making further penetration nearly impossible.
What is the best type of coolant for drilling stainless steel?
High-pressure neat cutting oils and heavy-duty semi-synthetic fluids with extreme pressure additives are the best coolants for drilling stainless steel. Extreme pressure (EP) additives containing sulfur or phosphorus react under friction to create a microscopic boundary layer that stops the drill bit from welding to the stainless steel. Products like Tap Magic Extra Thick or Castrol Ilocut perform exceptionally well for manual hole making. For closed CNC machinery, chlorinated or sulfurized water-miscible emulsions balance lubrication with high heat extraction.
How do I apply cutting fluid when drilling stainless steel on a drill press?
Apply cutting fluid to stainless steel by delivering continuous flow from a squeeze bottle or brush directly where the drill point enters the metal. Set your drill press to run at roughly 30 to 50 surface feet per minute (SFM) with steady, deliberate downward pressure. Peck drill repeatedly by backing the bit out every few millimeters to let fluid flood the hole and clear packed swarf. Keep a constant wet puddle around the hole circumference throughout the entire cut to stop the stainless steel from work hardening.
How do you mix water-soluble coolant for drilling stainless steel?
Mix water-soluble coolant by pouring the oil concentrate into water while stirring continuously, never adding water directly into oil. Pouring oil into water creates a stable chemical emulsion rather than an inverted, oily mixture that quickly separates. Use clean tap water or deionized water to prevent bacteria growth and mineral deposits. Check your finished batch using an optical refractometer before filling your workshop sump or spray bottle to ensure the oil droplets are evenly distributed.
Is neat cutting oil or water-soluble coolant better for drilling stainless steel?
Neat cutting oil is better for slow, manual drilling operations, whereas water-soluble coolant is superior for high-speed production drilling on CNC machines. Neat oil provides extreme lubricity, which preserves cutting edges at speeds under 40 surface feet per minute on standard drill presses. Water-soluble emulsions contain roughly 85 to 90 percent water, giving them far superior heat absorption for continuous drilling cycles above 800 RPM. For general workshop maintenance and deep hole drilling, straight sulfurized oil yields longer bit life.
What concentration of water-soluble coolant is required for drilling 304 and 316 stainless steel?
A coolant concentration between 10 percent and 15 percent is recommended when drilling 304 and 316 stainless steel. Standard machining of mild steel only requires a 5 to 7 percent mix, but stainless steel demands higher oil and additive ratios to handle severe tool friction. Measure the coolant mixture daily with a handheld refractometer and multiply the reading by your coolant’s specific refractive index factor. Running below 10 percent leads to torn threads, work hardening, and premature drill chipping.
Why is my drill bit smoking and overheating when drilling stainless steel?
Drill bits smoke and overheat in stainless steel when cutting speed is too high, feed pressure is too light, or coolant delivery is insufficient. Stainless steel work hardens immediately if a drill rubs instead of carving chips, quickly generating temperatures past 1,000 degrees Fahrenheit. Lower your drill spindle speed by half, increase your downforce until thick curls form, and submerge the hole entrance in high-lubricity cutting oil. If the drill tip has already turned blue or squeals, sharpen or replace the bit before continuing.
Can you safely use WD-40 as a coolant for drilling stainless steel?
WD-40 is not recommended as a drilling coolant for stainless steel because it lacks extreme pressure additives and creates a severe workshop fire risk. Standard WD-40 is a solvent-based water displacer with a low flash point of approximately 122 degrees Fahrenheit (50 degrees Celsius). Drilling stainless steel produces temperatures high enough to vaporize the light solvent, producing noxious fumes and potential flash fires. Use dedicated heavy cutting paste or extreme-pressure sulfurized cutting oil instead to ensure safe, smoke-free cutting.
