
7 Best Welding Wires For Galvanized Steel Old Farmers Swear By
Explore 7 welding wires for galvanized steel that old farmers swear by. This guide covers top choices for reducing porosity and ensuring strong, durable welds.
Youre standing in a muddy pasture with a broken gate hinge and a storm rolling in, realizing that welding galvanized steel is a different beast than clean mild steel. The zinc coating that protects your equipment from rust becomes your worst enemy under an arc, creating spitting, popping, and dangerous fumes. Choosing the right flux-core wire is the difference between a structural fix that lasts a decade and a brittle weld that snaps the next time a cow leans on it.
Disclosure: As an Amazon Associate, this site earns from qualifying purchases. Thank you!
Lincoln Electric Innershield NR-211-MP Flux-Core Wire

This wire is the undisputed heavy hitter in the farm shop for a reason. It is an all-position wire, meaning you can weld a vertical fence post just as easily as a flat bracket on a trailer. It handles the impurities found in galvanized coatings better than almost anything else on the shelf.
The "MP" stands for multi-pass, which is vital when you are building something substantial like a heavy-duty squeeze chute. While some wires get brittle if you lay down more than one bead, this Lincoln wire stays ductile and strong. Its a forgiving choice for the farmer who hasn’t picked up a torch in six months.
- Best for: Structural repairs and multi-pass welds.
- Tradeoff: It can be pricier than off-brand spools, but the reduced cleanup time usually pays for itself.
Hobart Fabshield 21B: The Standard for Farm Repairs

If you ask a neighbor what they use for fixing a rusted-out spreader, theyll likely point to a spool of 21B. This wire is engineered to have a very stable arc, which helps "burn through" the zinc layer to reach the base metal. It produces a soft arc that minimizes the violent spatter often associated with galvanized projects.
The slag on a 21B weld usually peels off with a simple tap of a chipping hammer. This is a huge advantage when you are working outside in the wind and can’t spend an hour grinding every joint. Its a reliable, "set it and forget it" wire for standard 110v or 220v MIG machines.
Blue Demon E71T-GS Gasless Wire for Zinc Coatings
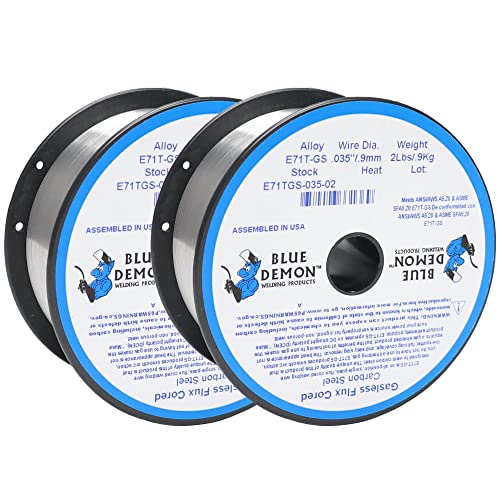
Blue Demon has gained a reputation for being the go-to wire for hobbyists who need professional results on a budget. Their GS (General Speed) wire is specifically designed for single-pass applications on thin-gauge galvanized steel. It runs exceptionally well on the small, portable flux-core welders found in most home shops.
Because it doesn’t require an external shielding gas, this wire is perfect for those "field hospital" repairs where you have to lug the welder out to the back forty. It handles the wind without losing its shielding properties. Just remember that it isn’t rated for heavy structural loads, so keep it to gates, brackets, and non-critical frames.
Forney 42300 Flux Core Wire for Rusty Galvanized Gates

Forney is a brand built for the agricultural community, and their 42300 wire reflects that heritage. It is particularly adept at handling "dirty" galvanized steelthe kind that has been sitting in a damp barn for twenty years. It has a high tolerance for surface contaminants that would make other wires porosity-ridden.
When you are welding an old gate, you often can’t get every bit of oxidation off the metal. This wire "wets out" the puddle nicely, ensuring the weld bonds to the steel rather than just sitting on top of the zinc. Its a gritty, hardworking wire for repairs that don’t need to be pretty, just permanent.
Harris E71T-GS Flux Cored Wire for Outdoor Projects

The Harris wire is a favorite for those who prioritize a smooth bead appearance even when working with difficult materials. It offers a very consistent diameter throughout the spool, which prevents the wire-feeding stutters that cause "cold laps" in your weld. This consistency is crucial when you are working with the unpredictable nature of galvanized coatings.
- Key Consideration: It produces very little smoke compared to other flux-core options.
- Application: Ideal for garden structures or decorative galvanized fencing where aesthetics matter.
While no flux-core wire is truly "smokeless," Harris manages to keep the mess to a minimum. This makes it easier to see your puddle, which is often the hardest part of welding galvanized steel. Better visibility leads to better penetration and a stronger overall repair.
INE E71T-GS Gasless Wire for High-Zinc Steel Repairs
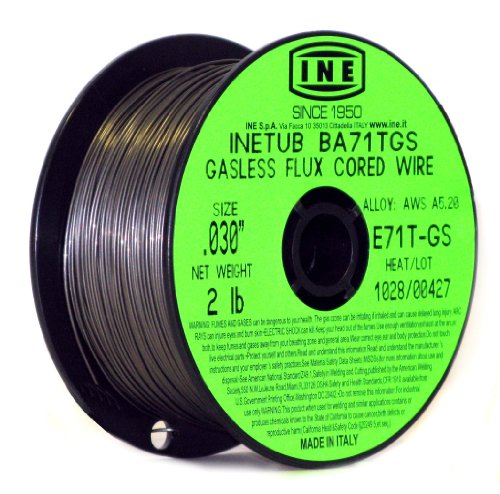
This European-made wire has become a sleeper hit among those who deal with heavy-duty hot-dipped galvanized components. Hot-dipped steel has a much thicker zinc layer than electro-galvanized sheet metal, which usually causes massive porosity issues. INEs formulation seems to "boil" the zinc out of the way more effectively than standard wires.
It creates a very fast-freezing puddle, which is a lifesaver when you are trying to fill a gap in a poorly fitted joint. On a farm, things rarely line up perfectly, and having a wire that can bridge a gap without falling through is a massive time-saver. Its a technical wire that performs like a simple one.
YesWelder E71T-GS Wire for Thin Galvanized Tubing
Modern farm equipment often uses thin-walled galvanized tubing because its light and cheap. The problem is that most welding wires run too "hot" and blow right through the metal. YesWelders wire is optimized for low-voltage settings, allowing you to stitch-weld thin tubing without creating a series of holes.
Its an excellent choice for repairing greenhouse frames or lightweight poultry housing. The arc starts easily even on lower-end machines, reducing the "stutter-start" that often ruins thin workpieces. If your project involves more sheet metal than heavy plate, this is the spool to reach for.
Safety Gear: 3M Respirators for Galvanized Welding
Welding galvanized steel isn’t just a mechanical challenge; its a health hazard. When zinc vaporizes, it creates white clouds of zinc oxide that cause "metal fume fever," a flu-like condition that can lay a person out for days. A standard dust mask will not protect you from these microscopic particles.
A 3M respirator equipped with P100 "pink" filters is the non-negotiable standard for this work. These filters are designed to capture the heavy metal fumes generated during the welding process. Even if you are working outside in a breeze, the eddies created by your welding hood can trap fumes right in your breathing zone.
- Fitment: Ensure the respirator fits under your welding hood comfortably.
- Maintenance: Change filters as soon as you smell anything through the mask or breathing becomes difficult.
- Environment: Always position yourself upwind of the weld, but never rely on the wind alone to keep you safe.
Success with galvanized steel comes down to respecting the chemistry of the coating and the physics of the weld. By matching the right wire to your specific repairwhether it’s heavy structural plate or thin-walled tubingyou ensure your hard work stays put. Always prioritize your lungs with a proper respirator, because no fence repair is worth a week of respiratory illness.
Frequently Asked Questions (FAQs)
What is the best welding wire for galvanized steel on a farm?
E71T-11 flux-cored welding wire is the most practical wire for repairing galvanized steel farm equipment in outdoor conditions. Old farmers prefer AWS classification E71T-11 or E71T-GS because these self-shielded wires burn through light zinc residues without requiring external gas bottles. For general fence gates and tractor attachments, 0.035-inch diameter wire provides balanced penetration on typical 1/8-inch carbon steel.
What does flux-cored wire do when welding galvanized metal?
Flux-cored wire releases internal chemical deoxidizers that vaporize and displace the zinc coating to prevent weld porosity. The core contains elements like aluminum and manganese that react with atmospheric contaminants and boiling zinc gas. As the steel melts at roughly 2,800 degrees Fahrenheit, the zinc boils off at 1,665 degrees Fahrenheit, allowing the flux slag to float impurities out of the weld puddle.
How do I prep galvanized steel before welding with flux core wire?
Grinding the zinc coating back at least one to two inches from the joint line is the proper way to prepare galvanized steel. Use an angle grinder equipped with a 36-grit flap disc or coarse wire wheel to expose bare silver steel. Once bare metal appears, wipe the joint with a dry rag to remove remaining zinc dust before striking your arc.
How do you stop porosity when welding galvanized pipe with solid wire?
Stopping porosity with solid wire requires grinding the weld zone completely clean and running an argon-carbon dioxide gas mix with slower travel speeds. Solid wires like ER70S-6 lack aggressive cleaning agents, making clean metal mandatory. Switch to a 75/25 argon and carbon dioxide shielding mix, step up your voltage slightly, and use a slight side-to-side whip to let zinc vapors escape.
Is flux core or solid MIG wire better for welding galvanized fence posts?
Self-shielded flux core wire is better than solid MIG wire for welding galvanized fence posts in field conditions. Fence repairs usually happen outdoors where wind blows away external MIG shielding gas, leading to brittle, sponge-like welds. Flux core wires tolerate light zinc remnants and breeze up to 30 miles per hour, whereas solid wire demands immaculate cleaning and windbreaks.
How much does a 10 pound spool of galvanized welding wire cost?
A 10-pound spool of flux-cored welding wire suitable for galvanized steel typically costs between $40 and $75. Brand-name wires such as Lincoln Innershield or Hobart Fabshield fall toward the upper end of that range, while generic E71T-GS spools cost less. Standard 0.030-inch and 0.035-inch diameters are the most economical sizes for farm shops and fit most standard wire-feed welders.
Why is my weld popping and blowing through galvanized sheet metal?
Excessive heat combined with rapidly boiling zinc causes welds to pop and blow through galvanized sheet metal. Zinc vaporizes at a much lower temperature than steel melts, creating pressurized gas pockets that explode as heavy spatter. If you are burning through thin 14-gauge or 16-gauge sheet, lower your machine voltage, increase wire speed slightly, and use short stitch welds instead of continuous beads.
Is it safe to weld galvanized steel without grinding off the zinc coating?
Welding directly over galvanized steel without grinding off zinc is dangerous because burning zinc releases toxic zinc oxide fumes that cause metal fume fever. Inhaling these dense white fumes leads to severe flu-like chills, nausea, headaches, and fatigue within 4 to 12 hours. Always grind the weld zone to bare steel, weld only in well-ventilated areas, and wear a half-mask respirator with P100 particulate filters.

